
工程背景
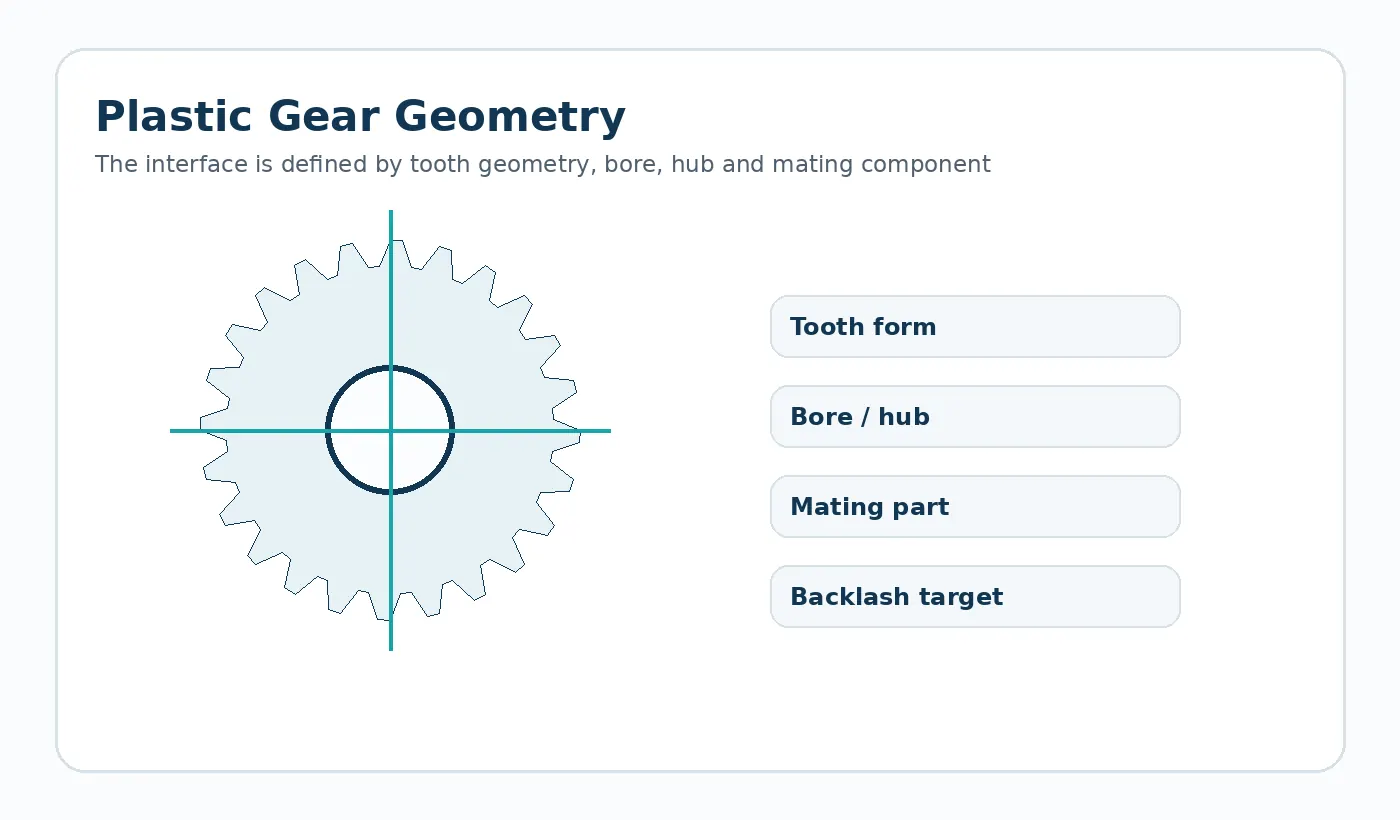
Secondary machining can refine bores, faces or datums after molding when the assembly needs a relationship that is difficult to hold directly from the tool.
The benefit must be weighed against extra handling, fixturing and the possibility of releasing molded-in stress. Machining also changes the datum chain if the gear tooth form remains as molded.
Secondary machining is most valuable when it controls a specific relationship that the molding process cannot hold economically. Typical candidates are precision bores, bearing seats or mounting faces. If the gear is fixtured from a cosmetic outer surface, however, machining may introduce a new eccentricity. The fixture should locate from a stable molded datum that has a known relationship to the teeth.
图纸需要传达的信息
Identify exactly which feature is machined, which molded surface locates the part in the fixture and which dimensions are inspected afterward.
尽可能将这些信息添加到受控图纸、规格说明或询价附件中。避免在非正式的沟通渠道中发布这些信息,有助于供应商比较和后续修改的管理。
风险评估
Adding a machined bore without a coherent tooth-to-bore datum can improve diameter size but not runout.
样品验收
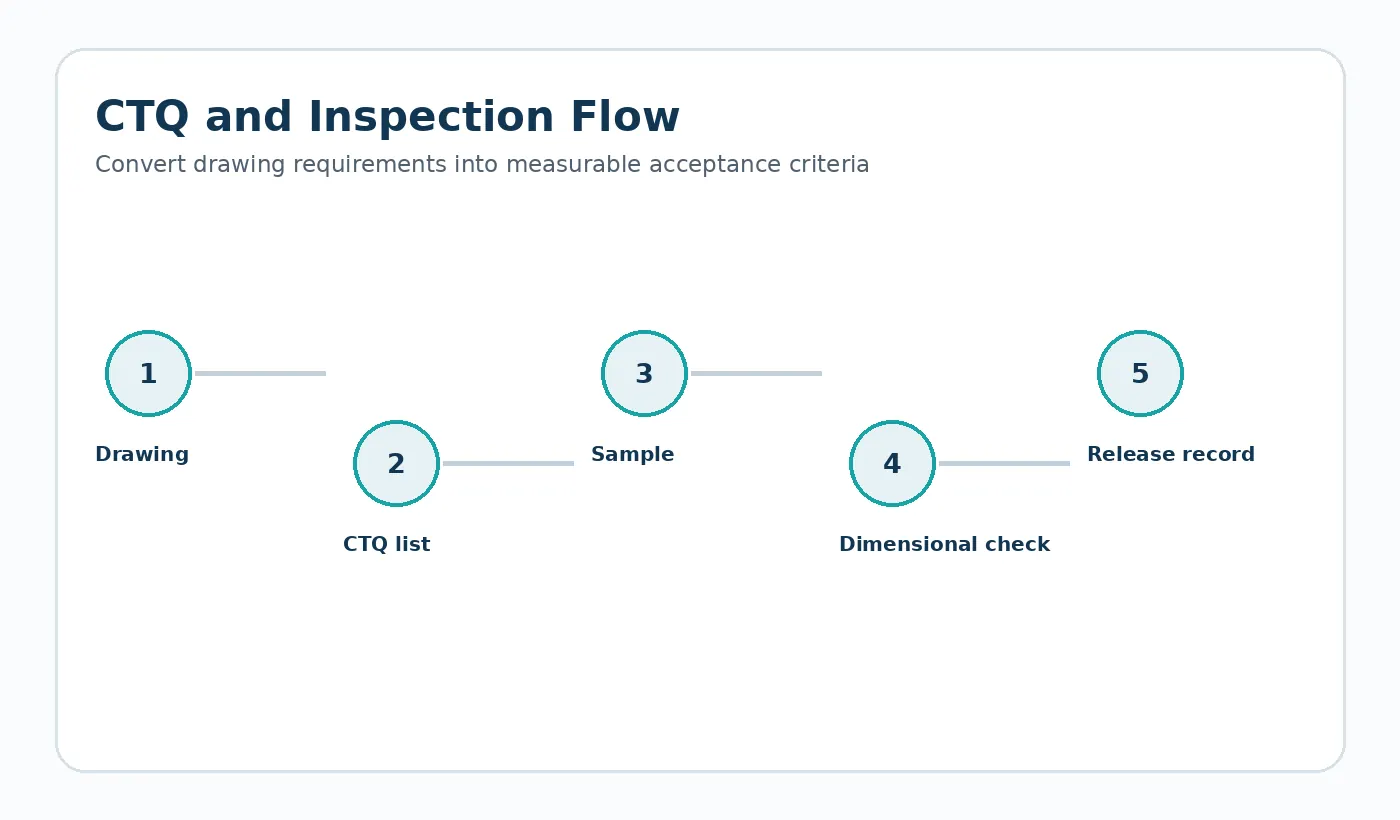
Use a fixture and inspection plan that references the functional gear datum structure.
For Secondary Machining of Molded Plastic Gears, close the DFM loop by updating the controlled CAD/drawing and sample plan. A recommendation that never reaches the released revision cannot be inspected consistently in production.
从设计评审到询价
Before requesting a price for secondary machining of molded plastic gears, identify the current drawing revision, production quantity, material constraint and the feature that most strongly affects function. Ask the supplier to flag any deviation from those inputs in the quotation so technical alternatives stay visible.
针对此决策的实用设计审查
Secondary machining can improve a final bore, datum, face or thread, but it changes the process chain. Define the datum used to locate the molded part, expected stock allowance, clamping method and how the machined feature relates to the gear teeth or molded interface.
将假设条件记录在图纸或询价单中,以便供应商在报价前进行确认。如果某个数值未知,应将其标识为待定工程项目,而不是直接复制可能与实际装配不符的通用产品目录编号。
验证工作表
- Molded datum used for setup
- Stock allowance
- Machined feature tolerance
- Clamp distortion risk
- Burr / stress / surface requirement
- Final inspection after machining
使用第一个样品,通过尺寸验证和相关的功能检查来确认这些要点。任何可接受的偏差都应在重复生产前的受控修订中记录下来。

























