
انجینئرنگ سیاق و سباق
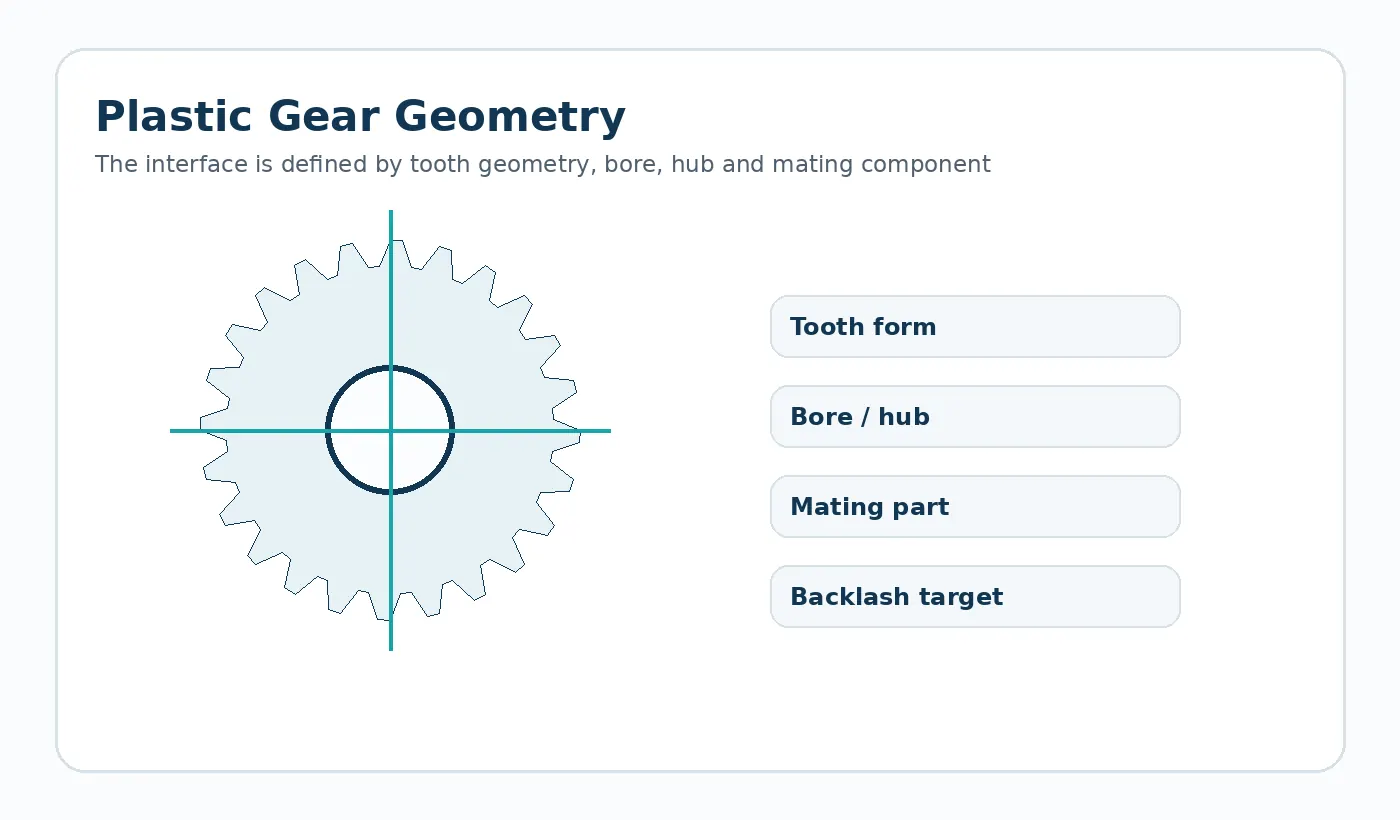
Secondary machining can refine bores, faces or datums after molding when the assembly needs a relationship that is difficult to hold directly from the tool.
The benefit must be weighed against extra handling, fixturing and the possibility of releasing molded-in stress. Machining also changes the datum chain if the gear tooth form remains as molded.
Secondary machining is most valuable when it controls a specific relationship that the molding process cannot hold economically. Typical candidates are precision bores, bearing seats or mounting faces. If the gear is fixtured from a cosmetic outer surface, however, machining may introduce a new eccentricity. The fixture should locate from a stable molded datum that has a known relationship to the teeth.
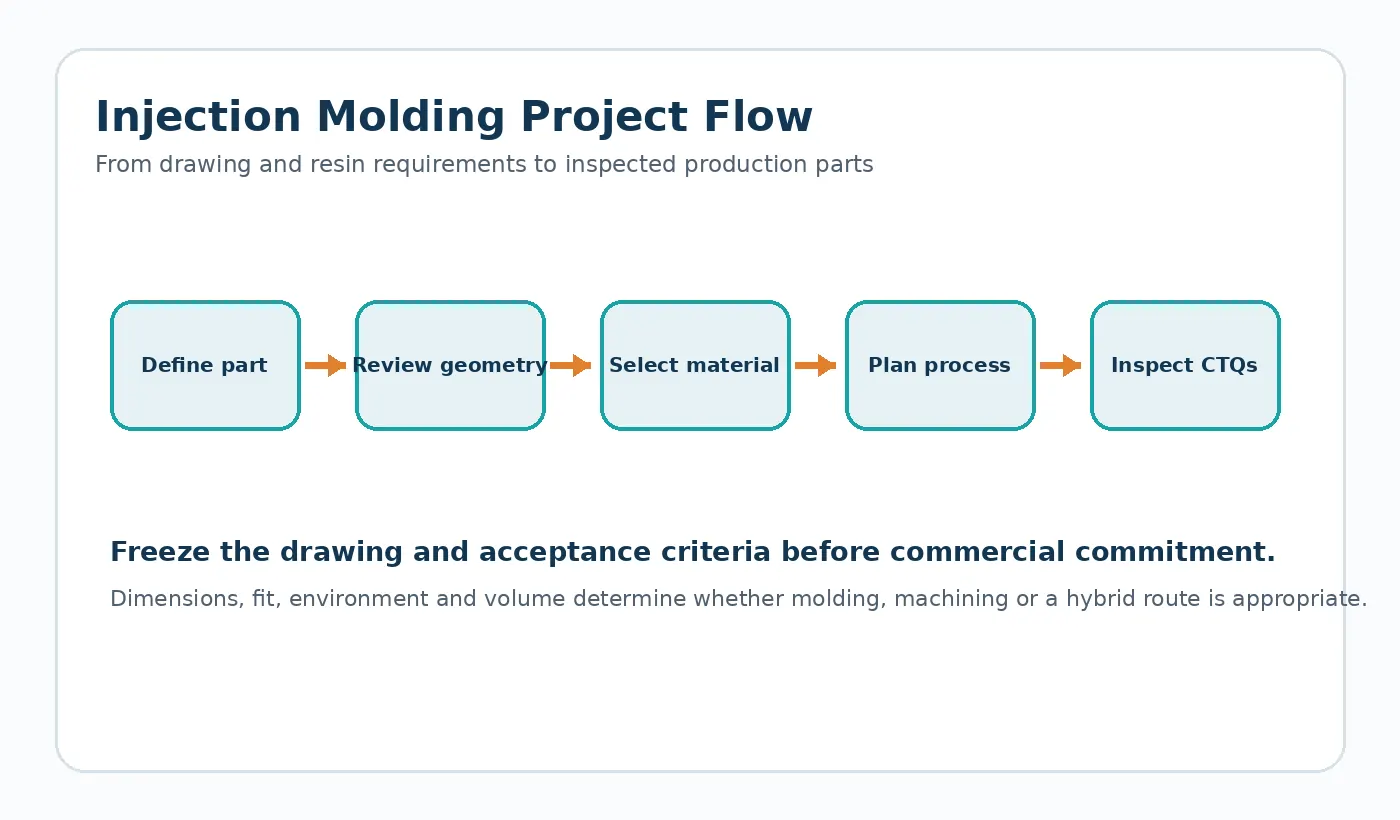
ڈرائنگ کو بات چیت کرنے کی کیا ضرورت ہے۔
Identify exactly which feature is machined, which molded surface locates the part in the fixture and which dimensions are inspected afterward.
ان پٹ کو کنٹرولڈ ڈرائنگ، تفصیلات یا RFQ منسلکہ پر جہاں ممکن ہو رکھیں۔ انہیں غیر رسمی پیغام کے دھاگوں سے دور رکھنے سے سپلائر کا موازنہ اور بعد میں نظرثانی کا انتظام کرنا آسان ہو جاتا ہے۔
خطرے کا جائزہ
Adding a machined bore without a coherent tooth-to-bore datum can improve diameter size but not runout.
نمونہ قبولیت
Use a fixture and inspection plan that references the functional gear datum structure.
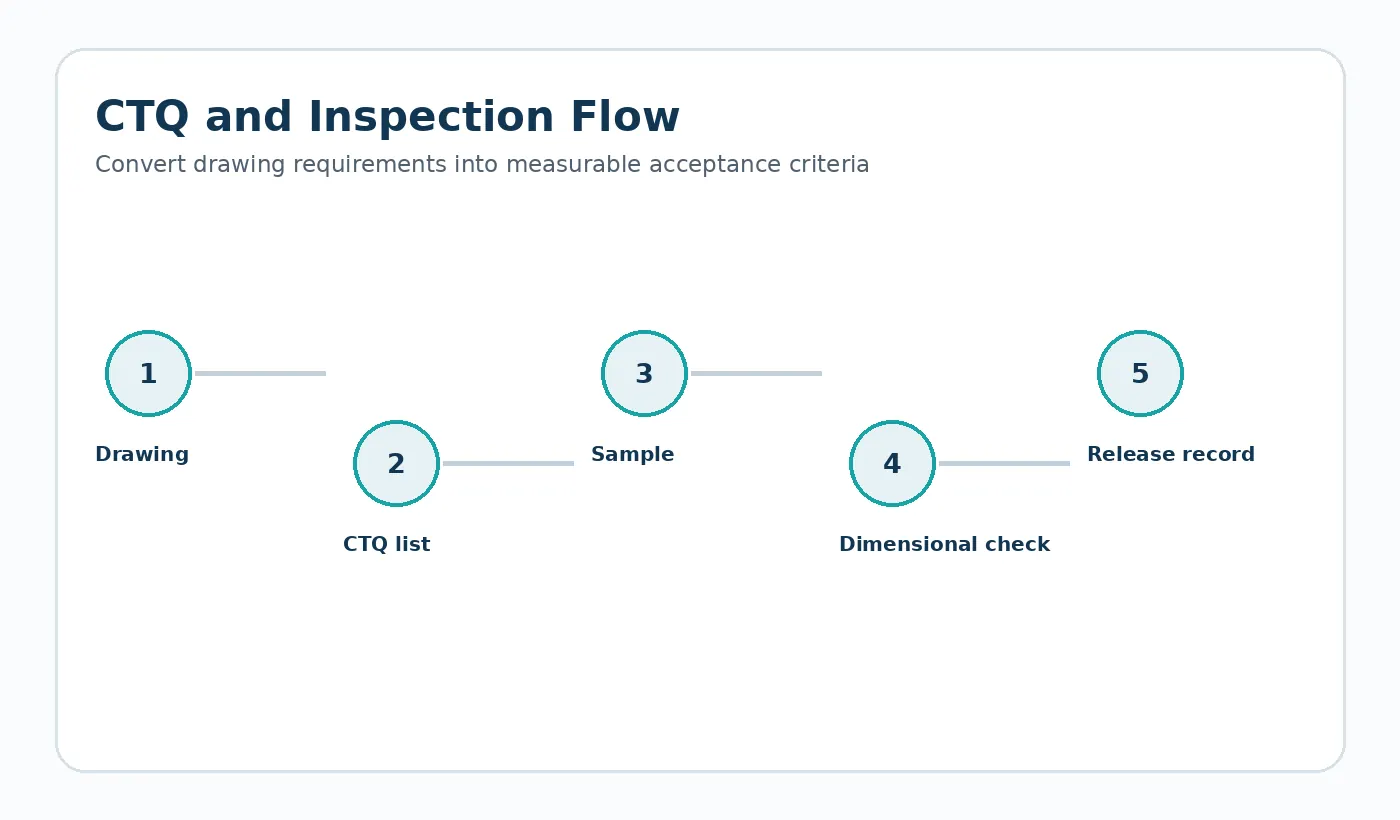
For Secondary Machining of Molded Plastic Gears, close the DFM loop by updating the controlled CAD/drawing and sample plan. A recommendation that never reaches the released revision cannot be inspected consistently in production.
ڈیزائن ریویو سے لے کر آر ایف کیو تک
Before requesting a price for secondary machining of molded plastic gears, identify the current drawing revision, production quantity, material constraint and the feature that most strongly affects function. Ask the supplier to flag any deviation from those inputs in the quotation so technical alternatives stay visible.
اس فیصلے کے لیے عملی ڈیزائن کا جائزہ
Secondary machining can improve a final bore, datum, face or thread, but it changes the process chain. Define the datum used to locate the molded part, expected stock allowance, clamping method and how the machined feature relates to the gear teeth or molded interface.
مفروضوں کو ڈرائنگ یا RFQ پر ریکارڈ کریں تاکہ سپلائر حوالہ دینے سے پہلے ان کی تصدیق کر سکے۔ جب کوئی قدر معلوم نہ ہو، تو اسے ایک عام کیٹلاگ نمبر کاپی کرنے کے بجائے ایک اوپن انجینئرنگ آئٹم کے طور پر شناخت کریں جو اسمبلی سے مماثل نہ ہو۔
تصدیقی ورک شیٹ
- Molded datum used for setup
- Stock allowance
- Machined feature tolerance
- Clamp distortion risk
- Burr / stress / surface requirement
- Final inspection after machining
جہتی ثبوت اور متعلقہ فنکشنل چیک دونوں کے ساتھ ان پوائنٹس کو بند کرنے کے لیے پہلا نمونہ استعمال کریں۔ کسی بھی قبول شدہ انحراف کو دوبارہ پیداوار سے پہلے کنٹرول شدہ نظرثانی میں پکڑا جانا چاہئے۔

























