
Engineering context
Secondary machining can refine bores, faces or datums after molding when the assembly needs a relationship that is difficult to hold directly from the tool.
The benefit must be weighed against extra handling, fixturing and the possibility of releasing molded-in stress. Machining also changes the datum chain if the gear tooth form remains as molded.
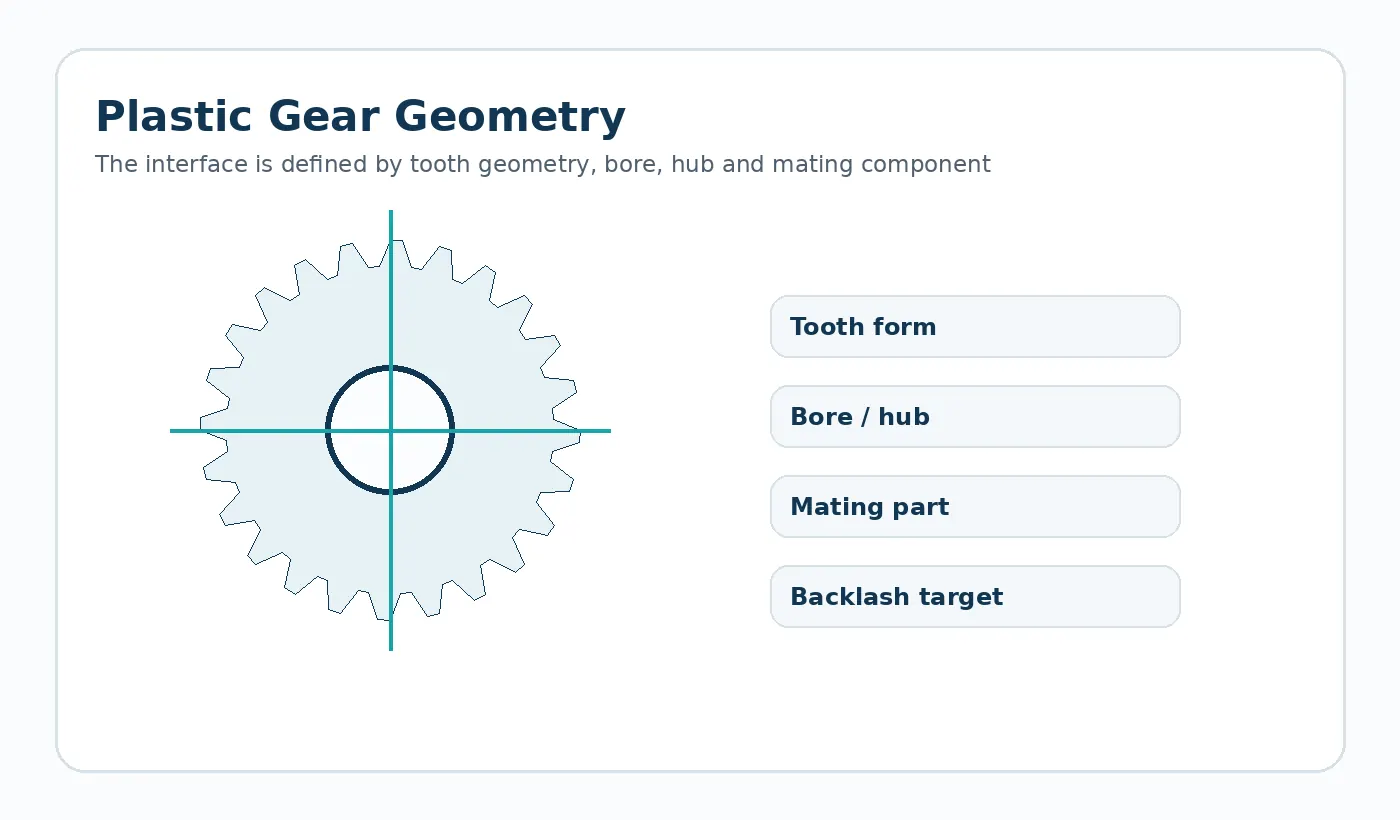
Secondary machining is most valuable when it controls a specific relationship that the molding process cannot hold economically. Typical candidates are precision bores, bearing seats or mounting faces. If the gear is fixtured from a cosmetic outer surface, however, machining may introduce a new eccentricity. The fixture should locate from a stable molded datum that has a known relationship to the teeth.
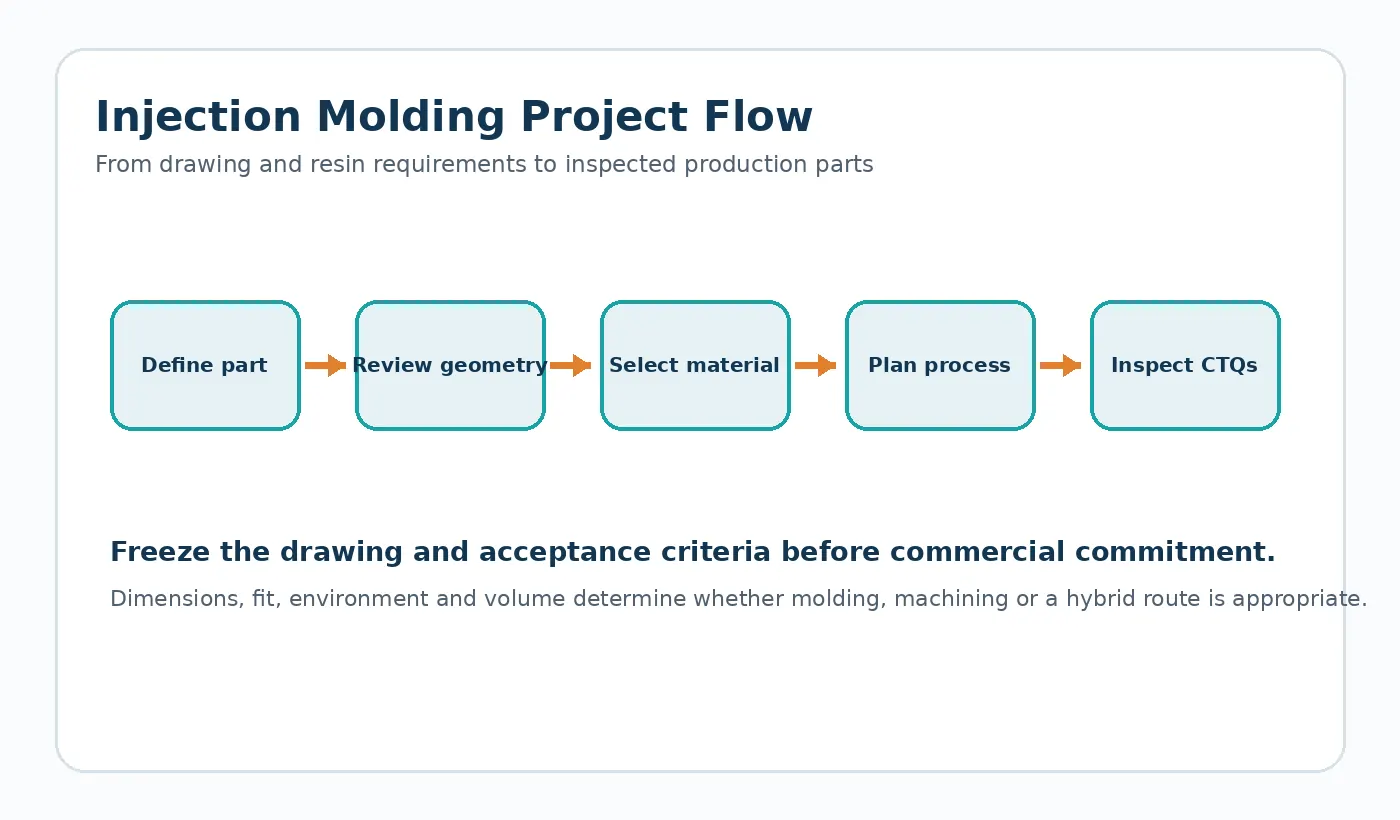
What the drawing needs to communicate
Identify exactly which feature is machined, which molded surface locates the part in the fixture and which dimensions are inspected afterward.
Cantumkan masukan-masukan ini pada gambar, spesifikasi, atau lampiran RFQ yang terkontrol jika memungkinkan. Dengan memisahkannya dari percakapan pesan informal, perbandingan pemasok dan revisi selanjutnya akan lebih mudah dikelola.
Risk review
Adding a machined bore without a coherent tooth-to-bore datum can improve diameter size but not runout.
Sample acceptance
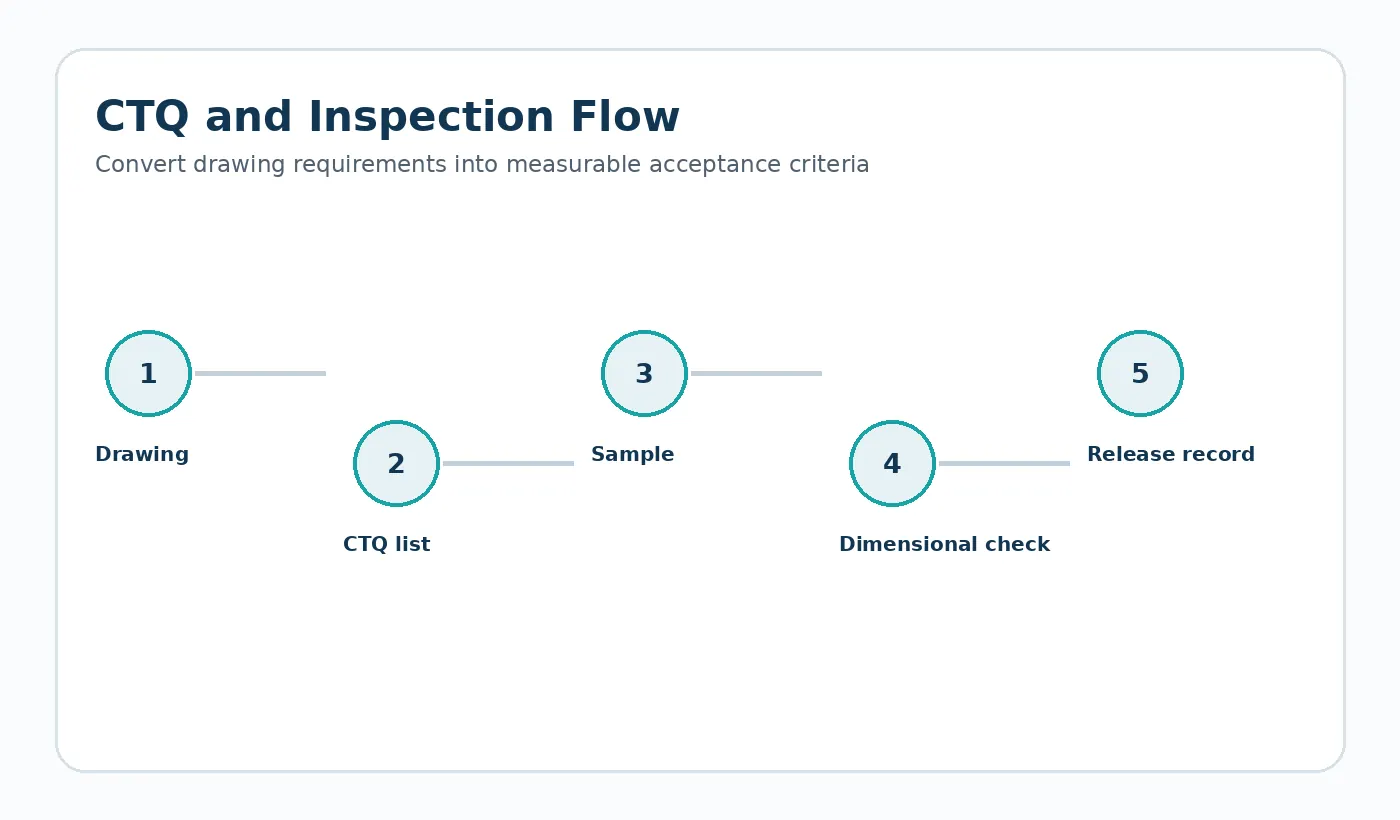
Use a fixture and inspection plan that references the functional gear datum structure.
For Secondary Machining of Molded Plastic Gears, close the DFM loop by updating the controlled CAD/drawing and sample plan. A recommendation that never reaches the released revision cannot be inspected consistently in production.
From design review to RFQ
Before requesting a price for secondary machining of molded plastic gears, identify the current drawing revision, production quantity, material constraint and the feature that most strongly affects function. Ask the supplier to flag any deviation from those inputs in the quotation so technical alternatives stay visible.
Tinjauan desain praktis untuk keputusan ini
Secondary machining can improve a final bore, datum, face or thread, but it changes the process chain. Define the datum used to locate the molded part, expected stock allowance, clamping method and how the machined feature relates to the gear teeth or molded interface.
Catat asumsi pada gambar atau RFQ agar pemasok dapat mengkonfirmasinya sebelum memberikan penawaran. Jika suatu nilai tidak diketahui, identifikasikan sebagai item rekayasa terbuka daripada menyalin nomor katalog umum yang mungkin tidak sesuai dengan rakitan tersebut.
Lembar kerja verifikasi
- Molded datum used for setup
- Stock allowance
- Machined feature tolerance
- Clamp distortion risk
- Burr / stress / surface requirement
- Final inspection after machining
Gunakan sampel pertama untuk melengkapi poin-poin ini dengan bukti dimensi dan pemeriksaan fungsional yang relevan. Setiap penyimpangan yang diterima harus dicatat dalam revisi terkontrol sebelum produksi ulang.

























