
Engineering context
Secondary machining can refine bores, faces or datums after molding when the assembly needs a relationship that is difficult to hold directly from the tool.
The benefit must be weighed against extra handling, fixturing and the possibility of releasing molded-in stress. Machining also changes the datum chain if the gear tooth form remains as molded.
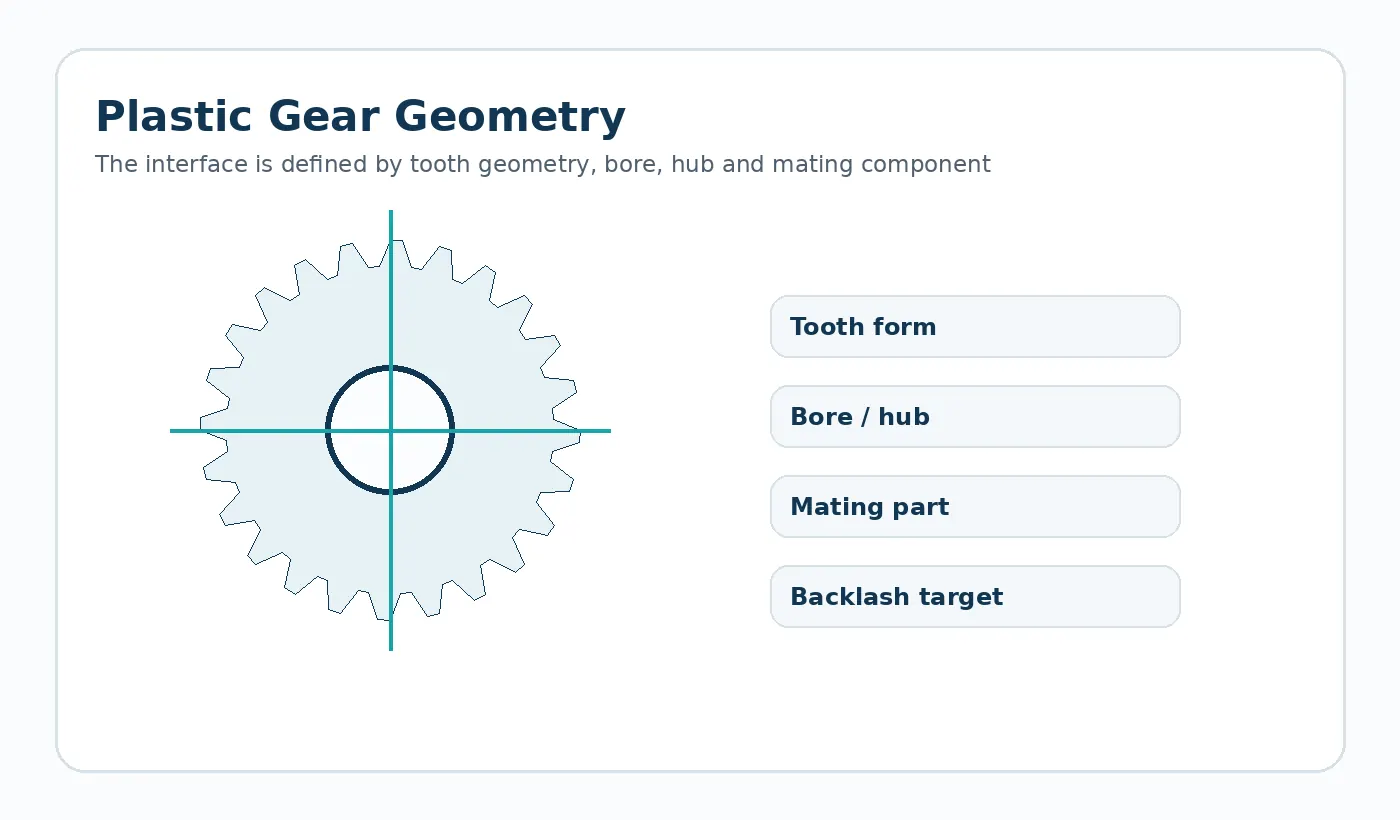
Secondary machining is most valuable when it controls a specific relationship that the molding process cannot hold economically. Typical candidates are precision bores, bearing seats or mounting faces. If the gear is fixtured from a cosmetic outer surface, however, machining may introduce a new eccentricity. The fixture should locate from a stable molded datum that has a known relationship to the teeth.
What the drawing needs to communicate
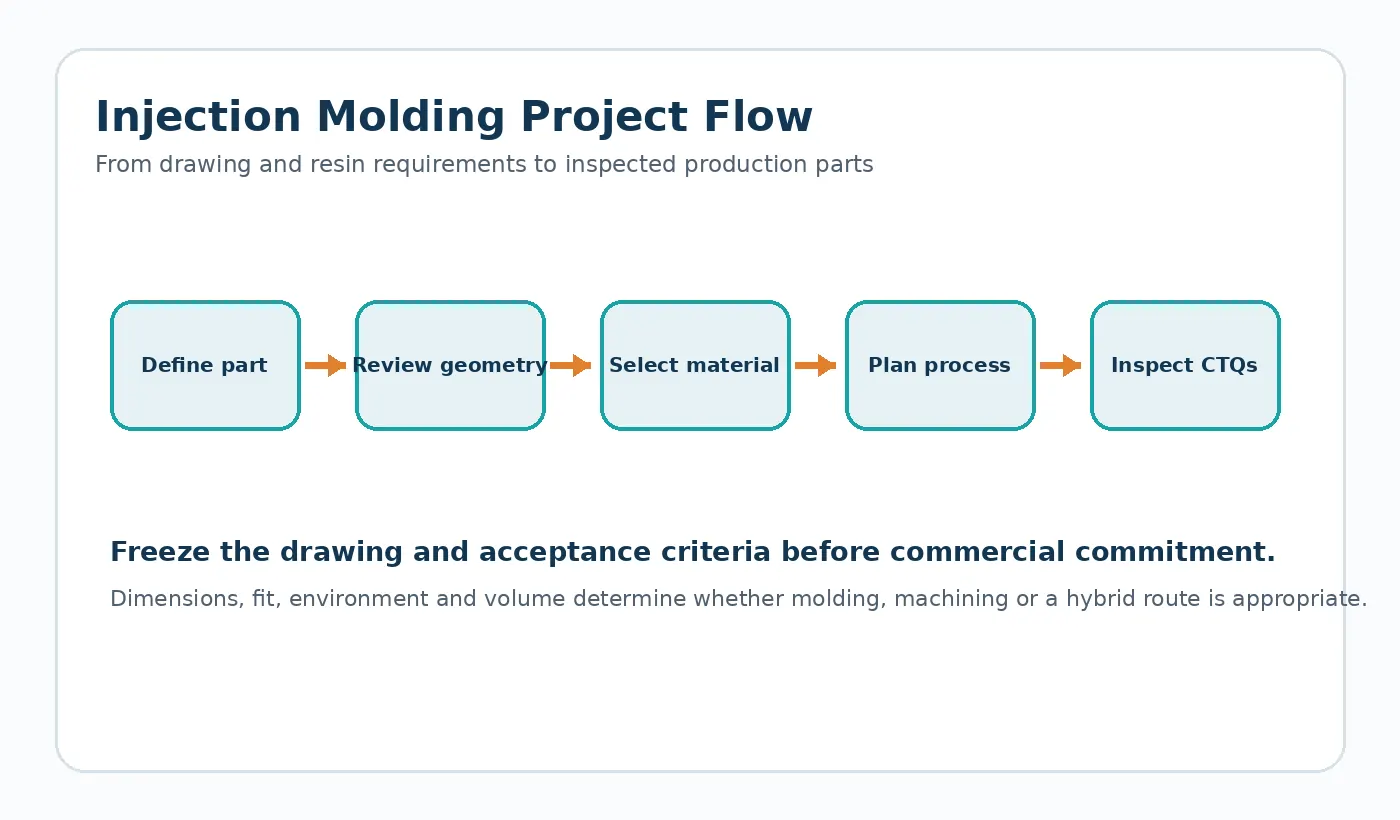
Identify exactly which feature is machined, which molded surface locates the part in the fixture and which dimensions are inspected afterward.
Incluya estos datos en el plano controlado, la especificación o el archivo adjunto de la solicitud de cotización, siempre que sea posible. Mantenerlos fuera de los hilos de mensajes informales facilita la comparación entre proveedores y la gestión de revisiones posteriores.
Risk review
Adding a machined bore without a coherent tooth-to-bore datum can improve diameter size but not runout.
Sample acceptance
Use a fixture and inspection plan that references the functional gear datum structure.
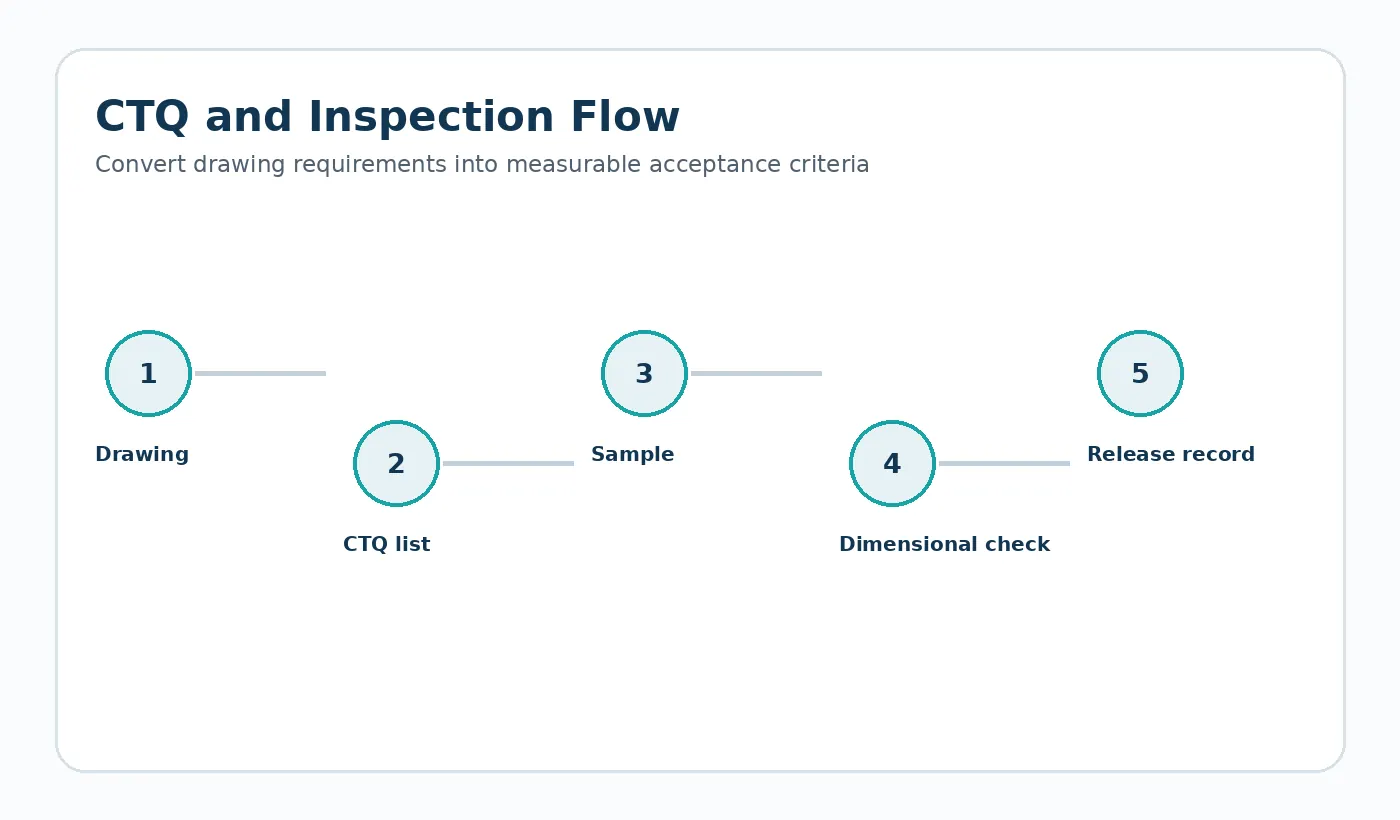
For Secondary Machining of Molded Plastic Gears, close the DFM loop by updating the controlled CAD/drawing and sample plan. A recommendation that never reaches the released revision cannot be inspected consistently in production.
From design review to RFQ
Before requesting a price for secondary machining of molded plastic gears, identify the current drawing revision, production quantity, material constraint and the feature that most strongly affects function. Ask the supplier to flag any deviation from those inputs in the quotation so technical alternatives stay visible.
Practical design review for this decision
Secondary machining can improve a final bore, datum, face or thread, but it changes the process chain. Define the datum used to locate the molded part, expected stock allowance, clamping method and how the machined feature relates to the gear teeth or molded interface.
Record the assumptions on the drawing or RFQ so the supplier can confirm them before quoting. When a value is unknown, identify it as an open engineering item rather than copying a generic catalogue number that may not match the assembly.
Verification worksheet
- Molded datum used for setup
- Stock allowance
- Machined feature tolerance
- Clamp distortion risk
- Burr / stress / surface requirement
- Final inspection after machining
Use the first sample to close these points with both dimensional evidence and the relevant functional check. Any accepted deviation should be captured in the controlled revision before repeat production.

























