
Quality planning should follow the function of the part
Inspection is most useful when it is tied to the characteristics that control assembly and service. Measuring every dimension with the same priority can add cost without reducing the actual project risk.
For a molded gear, that may mean bore location, tooth geometry, runout and mesh behavior. For a housing, it may mean datum relationships, mounting surfaces, insert position and critical envelope dimensions.
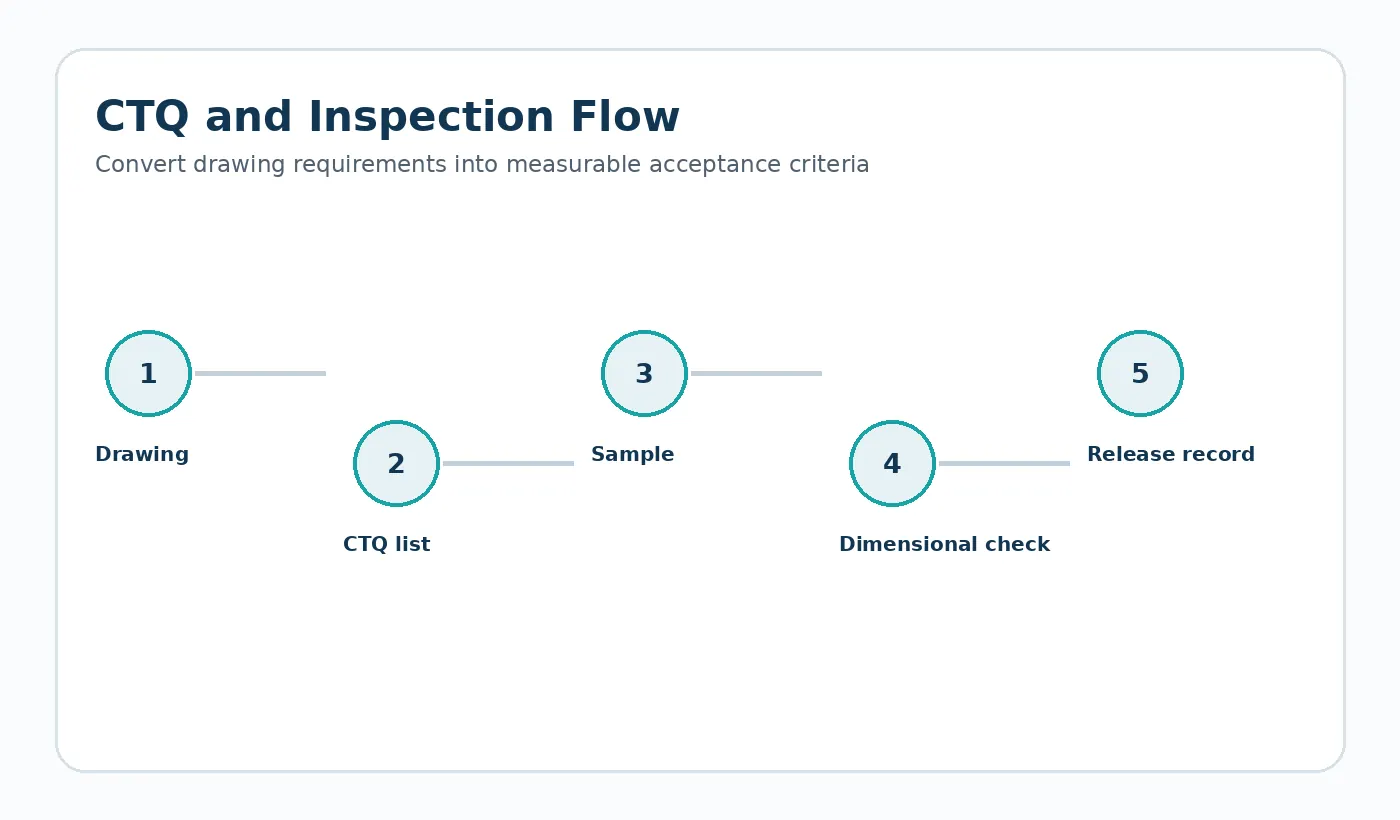
Define acceptance before repeat production
Drawing control
Use a clear revision, datums, tolerances and notes that match the intended inspection method.
Sample approval
Agree which characteristics are checked dimensionally and which require assembly or functional evaluation.
Production monitoring
Choose checks that can detect process drift in the features that matter to the application.
Choose measurements that reflect assembly function
A bore that locates a gear on a shaft may deserve a different inspection strategy from an exterior surface that only clears a cover. Likewise, a long rack needs pitch and straightness control along its travel, while a housing may depend on the relationship between mounting holes and a bearing seat.
Critical-to-quality planning ranks these relationships before production. It does not mean every dimension is tightened; it means the measurement effort is aimed at the features that can change the mechanism.
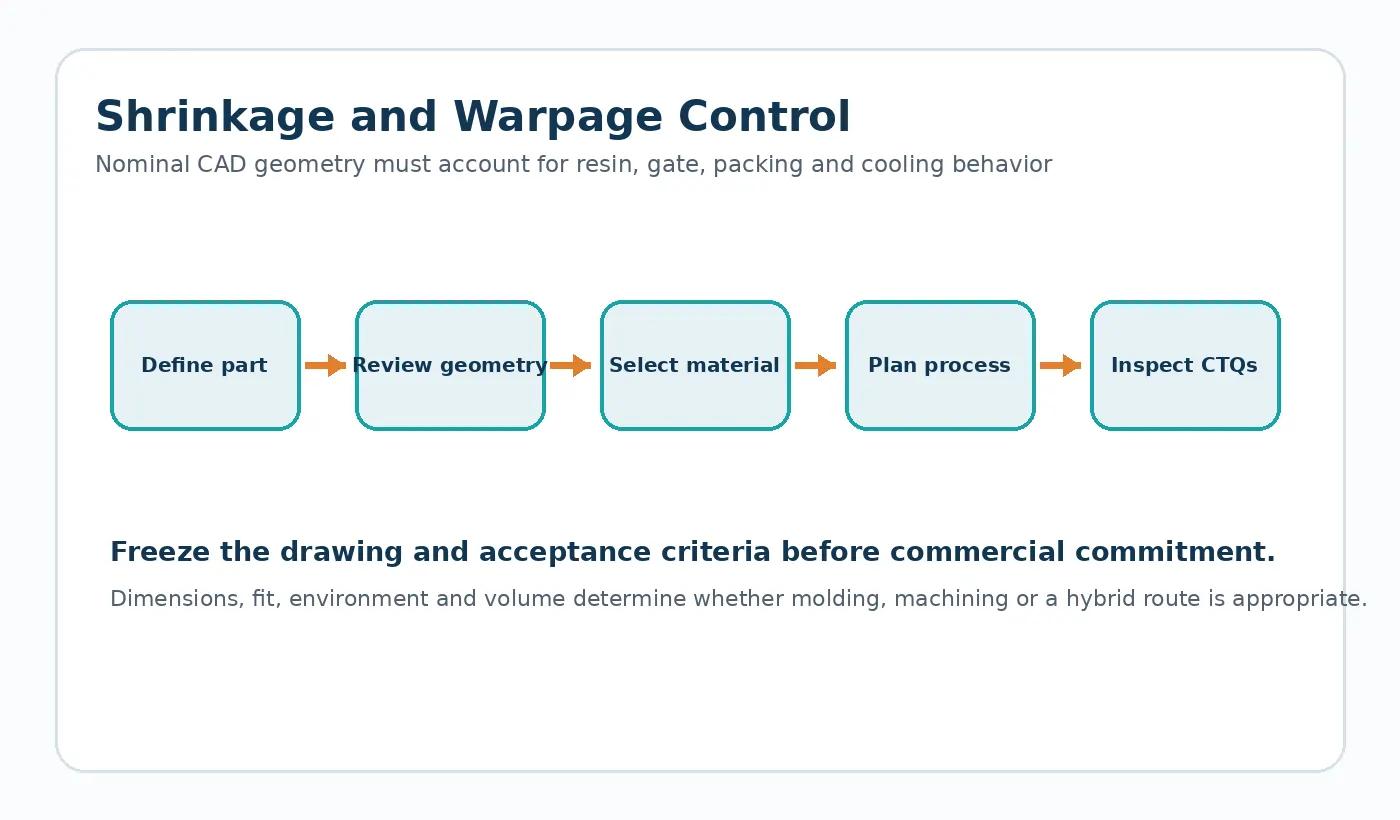
Plastic dimensions depend on condition
Temperature and moisture can change the dimensions of engineering polymers. Inspection records are more useful when the part condition is defined for sensitive features. For nylon components, conditioning may be especially relevant; for assemblies that combine plastic with metal shafts or housings, thermal expansion differences can alter fit or center distance.
Where a functional gauge or assembly check is used, document the mating condition and acceptance rule. This turns a subjective “fits well” judgement into a repeatable production check.
Evidence to agree before production
- Drawing revision and datum scheme
- Critical dimension list or inspection characteristic matrix
- Material/grade record
- Sample quantity and measurement condition
- Functional mesh, fit or assembly test where relevant
- Change-control route for approved deviations
Inspection must reproduce the drawing definition
Agree datum setup, instrument type and conditioning state for CTQs before first-article inspection. Flexible or moisture-sensitive polymer parts can give different results when fixtured, conditioned or measured differently, so the method is part of the specification for close-tolerance features.
Production control should focus on features with a plausible process failure mode: tooth-to-bore runout, rack straightness, insert position, critical wall transitions, hub fit, mating distance or other interface dimensions. Cosmetic checks belong in a separate visual standard when appearance matters.

























